

Thermal-Spray Wire for Existing Coating Equipment
Choose replacement spray wire by the coating you need and the feed system you already run. This guide connects zinc, zinc-aluminium and aluminium chemistry with diameter, winding and package fit, then separates a smooth feeding trial from coating acceptance. Use it to define one compatible consumable package before comparing repeat-supply offers.
Start from the specified coating metal
If you are qualifying replacement thermal-spray wire for an existing gun, start with the approved coating composition and the machine's actual feed specification. Select zinc, a defined zinc-aluminium alloy or aluminium from the coating design, then verify diameter, condition and spool/drum interface. Relia supports feedstock supply and selection; steel-wire production does not establish every spray-metal manufacturing route. Send the gun and accepted-wire references so the proposed material can be checked through a feed and coating trial before repeat supply is released.
- Zinc wireUse when the coating specification selects zinc with defined impurity limits.
- Zinc-aluminium wireChoose one alloy ratio before checking the actual feed diameter.
- Aluminium wireMatch the selected composition and physical condition to the coating system.
Selection context and decision detail
| Buyer requirement | Relia response | Evidence / condition |
|---|---|---|
| Defined coating chemistry | Spray-wire supply and selection | One metal/alloy and impurity specification |
| Compatible continuous feed | Diameter/condition/package review | Actual gun, drive and payout interface |
| Repeatable qualification | QC and batch-record scope agreed | Feed trial plus deposited-layer acceptance |
Feedstock supply should identify material and producer responsibility
Identify the actual feedstock producer and the chemistry, diameter and packaging represented by the offer.
Relia supports zinc, zinc-aluminium and aluminium spray-wire supply and selection. Their melting, alloying and wire-production routes are not confirmed as in-house from the steel-wire manufacturing fact. Company incoming, in-process and final QC and corresponding batch records are confirmed; agree the actual producer and represented chemistry/geometry evidence.
The zinc reference has an actual 4.35 mm entry versus a 2.0 mm title request. The ZnAl title names several compositions while the option says ZN. The aluminium reference has a broad 1.2–5 mm option. Each needs one compatible material/diameter selection.
- SystemApproved coating-material requirement
- EquipmentModel and applicable wire guidance
- ProposalActual material and feed format
Coating composition must come before a purity comparison
Select zinc, a defined zinc-aluminium ratio or aluminium from the coating requirement before comparing purity.
Turn the coating identity into material evidence
Pure zinc, a selected ZnAl ratio and aluminium are different feedstock identities. Choose the required chemistry from the coating specification, including relevant impurity limits, rather than rank them by a single generic purity number.
A pure-zinc minimum cannot describe every ZnAl alloy. Material analysis and physical dimensions should be represented by the actual lot, not inferred from silver colour.
- Coating requirementName the metal or alloy ratio required by the coating design.
- Chemistry evidenceCompare represented lot composition with the selected limits and impurity requirements.
- Physical identityRecord the wire diameter and package separately from the chemistry result.
Product references for your shortlist
Open the product details, then discuss the exact specification for your application.
Zinc thermal-spray wire
A zinc-feedstock enquiry starting point when the approved coating system calls for zinc rather than an alloy.
Zinc-aluminium spray wire
A candidate for a specified ZnAl coating composition, selected separately from wire size and feed format.
Aluminium thermal-spray wire
A candidate when the coating design selects aluminium and the existing feed system can accept its offered format.
Diameter and surface condition govern the feed interface
Match diameter, surface condition and winding to the rollers, guides and contact hardware actually installed.
Verify the actual diameter and limits against rollers, guides and contact hardware. Kinks, inconsistent section, surface contamination or damaged winding can interfere with feeding even when the nominal alloy is correct.
Specify cast/helix or straightness assessment where the equipment requires it, with the feed format and method stated. A broad diameter range does not qualify every gun.
- Diameter controlMatch actual size and limits with the rollers, guides and contact hardware.
- Surface and sectionInspect kinks, inconsistent section and contamination that can interrupt continuous delivery.
- Winding requirementDefine the feed format and any equipment-required cast, helix or straightness assessment.
The deposition process needs continuous compatible feeding
Identify arc or flame spraying first because their heat sources and feed arrangements differ.
In twin-wire arc spraying, wire tips melt at an arc while an air stream transports atomized metal. Inconsistent feeding can change process stability, so consumable evaluation must include the actual drive and wire path.
Wire flame spraying uses a different heat source and feed arrangement. Confirm the installed process rather than assume one trial covers both systems.
- IdentifyInstalled spray process and hardware
- FeedDefined diameter, condition and format
- ObserveStable payout and process behavior
- AssessRequired coating evidence separately
Spool or drum geometry is an equipment condition
Specify spool or drum dimensions and payout requirements rather than selecting a package by appearance.
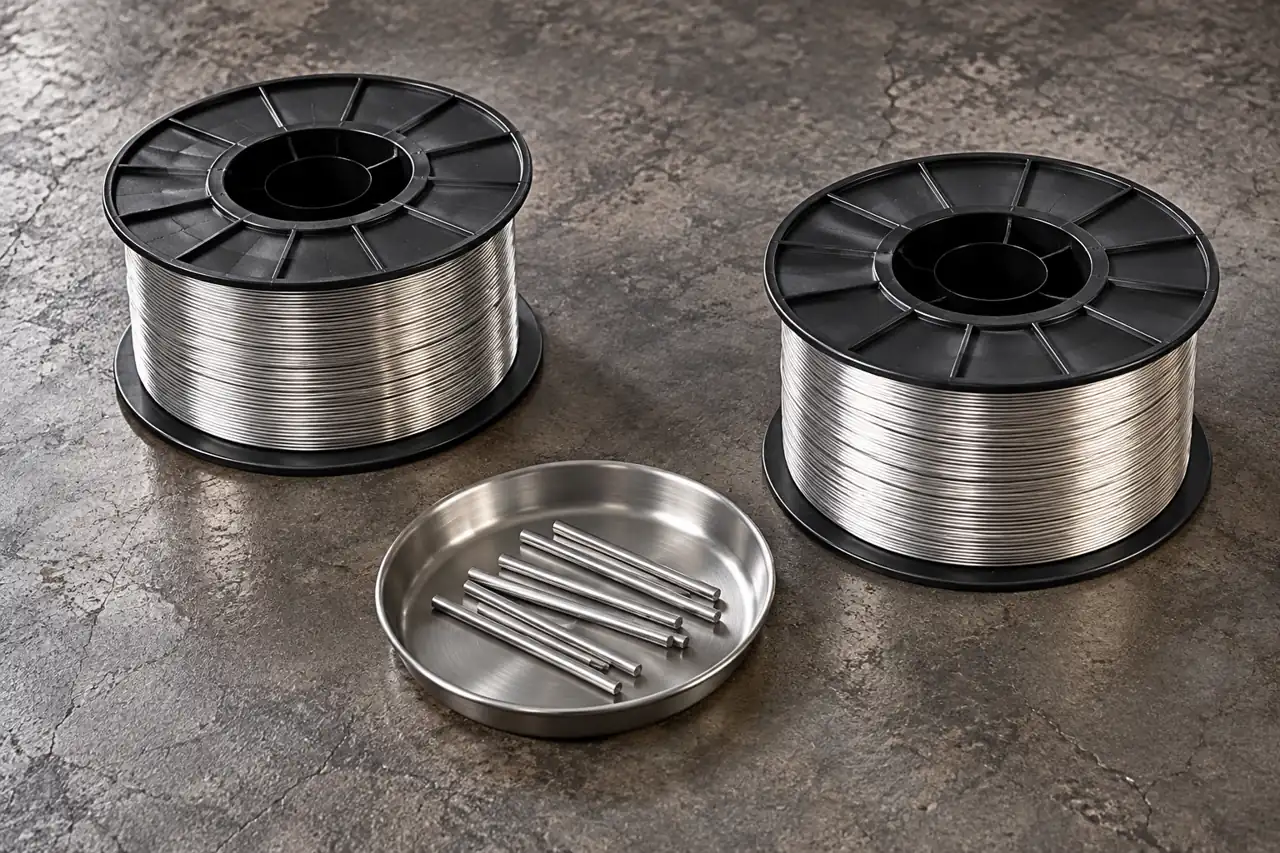
Check the package at the feed unit
Specify bore, flange/envelope, handling limits and payout arrangement for the actual feed unit. The catalogue's drum descriptions and spool illustrations are alternatives to confirm, not a guarantee that all packages are available.
Retain packaging identity after opening and record whether a feed issue occurs at a particular winding position or handling event.
- Package envelopeConfirm bore, flange dimensions and handling limits against the installed equipment.
- Payout arrangementDescribe the wire path and how the package feeds the drive.
- Winding conditionRetain lot identity and record any feed problem by winding position.
A replacement trial should compare both feeding and coating
Judge feed stability and deposited-coating acceptance separately under one recorded equipment and preparation baseline.
Use the intended gun, hardware, substrate/preparation and coating acceptance. Record wire lot, feed behavior and operating conditions, then assess the required deposited-layer characteristics separately.
A stable arc does not alone establish adhesion or service suitability. Compare candidates under a controlled baseline instead of changing preparation and wire together.
- MaterialOne chemistry and lot
- PhysicalDiameter, surface and winding
- MachineActual hardware and setup
- CoatingPrepared sample and accepted layer result
Lot records should answer chemistry and physical questions separately
Keep chemistry evidence separate from geometry and feed-condition checks, with both linked to the lot.
Keep the two acceptance records connected
Request represented composition, selected diameter and agreed surface/feed-condition evidence. Keep the material specification and packaging revision linked to the actual lot and trial.
The confirmed QC stages do not specify a particular chemistry instrument, inspection frequency or automatic ISO/GB compliance. The applicable technical supply basis must be selected and verified.
- Material recordIdentify the selected chemistry and the actual lot represented by analysis.
- Feed recordRecord diameter, surface condition and winding against the agreed equipment requirements.
- Trial referenceLink both records with the tested setup and coating acceptance decision.
Repeat supply should preserve the qualified consumable package
Preserve the qualified chemistry, diameter, winding and package when reviewing repeat lots or producer changes.
Carry forward chemistry/impurity limits, diameter, condition, feed format and the accepted equipment setup. Review changes in producer or package before treating a new lot as a routine substitute.
The retained short samples illustrate material comparison, not a finished shot product; the loose-wire image does not recommend unprotected outdoor storage.
- ApproveComposition, diameter, package and trial
- ReceiveIdentity and agreed material checks
- ReviewChanges before loading the wire
Build a compatible spray-wire enquiry
Send the gun interface, accepted coating specification and current consumable evidence for a focused replacement review.
Share the coating requirement and the equipment interface you need to preserve. We can review one proposed feedstock package and the trial evidence needed for approval.
Qingdao Relia Industries Co., Ltd.
Contact address: Shuyuan Road, Qingdao, Shandong, China
- Gun model and feed hardware
- Selected coating metal or alloy
- Wire diameter and feed format
- Current wire and trial evidence
Enquiry scope and supporting detail
Send process/gun model, current wire designation and diameter, rollers/guides, feed format and the coating specification. Include representative feed or coating problems and the evidence used to accept the existing material. We can then define one proposed wire package and a meaningful qualification trial, with producer responsibility and repeat-order terms agreed.
- CoatingMaterial and composition requirement
- FeedDiameter, equipment and spool format
- SupplyTrial quantity, records and destination