

ER70S-6 Welding Wire for Carbon Steel Fabrication
Select an ER70S-6 consumable around the welding procedure and feeder your fabrication shop actually uses. This guide connects documented classification, wire diameter and copper-coated delivery with a representative joint trial. It helps you separate a feed interruption from a shielding or preparation problem and retain the right evidence when approving a replacement supply.
Approve the consumable through the actual joint
For carbon-steel fabrication using gas-shielded solid wire, buy a documented ER70S-6 consumable identity with the required diameter, surface and spool arrangement for the approved welding procedure. A copper-coloured wire or a shared classification title does not establish every deposited-metal or joint property. Relia manufactures steel wire and can discuss the listed welding-wire enquiry and corresponding batch evidence. Start with parent material, joint/thickness, required filler designation, shielding gas and feeder. Qualify feed stability and the required weld results under recorded conditions before adopting a different producer, wire size or commercial pack.
- Procedure requirementIdentify the required filler designation, gas and actual parent joint configuration.
- Wire packageSelect diameter, copper-coated condition and a carrier compatible with the feeder.
- Trial acceptanceRecord delivery behaviour and the required joint examinations as separate conclusions.
Selection context and decision detail
| Buyer requirement | Relia response | Evidence or condition |
|---|---|---|
| Gas-shielded solid filler | Review a defined ER70S-6 offer | Classification, gas and procedure basis must be documented |
| Manufacturing/evidence | Confirmed wire operations and staged batch records | Actual consumable producer and copper surface identified |
| Usable fabrication input | Discuss diameter and winding | Feeding and joint results assessed separately |
Wire manufacturing evidence must identify the actual consumable
Identify the actual consumable producer, copper-coated surface and classification records within the selected welding-wire offer.
Relia's in-house steel-wire operations include drawing, annealing and galvanizing, with incoming, process and final inspection and corresponding batch records available. For this welding-wire item, identify the actual consumable producer, wire route, copper-coated surface and classification evidence in the offer. General galvanizing capability does not describe the selected copper coating.
The company manufacturing scope does not establish a particular welding certification, approval society or procedure. Request the records applicable to the offered batch and the classification required by your fabrication programme.
- Wire manufacturingConfirmed core processes
- Consumable offerProducer, classification and copper surface
- EvidenceCorresponding batch records and required approvals
Classification references need a coherent documented offer
Resolve the required classification and diameter as one documented consumable rather than combining several family references.
The catalogue combines EN ISO14341, EN440 and G46 4M G3Si1 wording with ER70S-6/ER50-6 model fields. Obtain evidence for the actual designation rather than treating the names as automatic equivalents. It describes a 0.8–1.6 mm range and CO2 shielding, but has no actual selectable variants.
State one diameter with limits and the intended winding/pack form. Broad 500 MPa low-alloy application wording is not a measured deposited-metal result. Certificate names in the entry do not prove current approval for the selected product or lot.
- AWS modelER70S-6 / ER50-6 wording
- EN titleISO14341 / G46 4M G3Si1 references
- DiameterDescribed 0.8–1.6 mm; no actual menu
- OrderOne selected documented consumable
Product references for your shortlist
Open the product details, then discuss the exact specification for your application.
Copper-coated ER70S-6 welding-wire enquiry
A consumable candidate to define by documented filler classification, selected diameter and the actual gas-shielded fabrication procedure.
Wire delivery and electrical contact affect the arc
Check guides, contact hardware and winding because continuous delivery and electrical contact both affect arc stability.
Locate an interruption in wire delivery
A continuously fed solid wire must pass guides and contact tips consistently while carrying current into the arc. Diameter variation, winding interruptions, surface debris or unsuitable guide/tip combinations can disturb that delivery. Copper coating is part of the selected surface condition, not proof of complete weld performance.
Define the actual diameter, surface and spool acceptance, then record wire feed, contact-tip/liner condition and process settings during the trial. Separate a mechanical feed stop from a gas or joint-preparation defect instead of changing the filler classification to correct every unstable result.
- Wire conditionCheck actual diameter, winding and surface for the trial spool.
- Feed hardwareRecord liner, guide and contact-tip condition with the observed feeding behaviour.
- Process contextRetain gas, preparation and settings before attributing every unstable result to filler chemistry.
Shielding and classification evidence have different scopes
Keep classification evidence separate from production-joint acceptance under the actual gas, parent material and procedure.
AWS A5.18 classification uses material and as-welded evidence under defined requirements. Actual production weld properties also depend on shielding, process conditions, parent-metal dilution and procedure. A test result under one gas cannot be silently applied to a different gas or transfer condition.
Use the required classification and welding procedure to define the applicable record and acceptance. Do not select amperage, voltage or a gas mixture from a generic catalogue description. The responsible welding team must validate the actual joint and operating envelope.
- ClassificationSpecified material/as-welded basis
- ProcedureParent joint, gas and process
- TrialRecorded conditions and wire identity
- AcceptanceRequired actual joint examinations
The coupon trial checks the intended fabrication result
Use representative joint coupons and required examinations rather than relying on bead appearance alone.
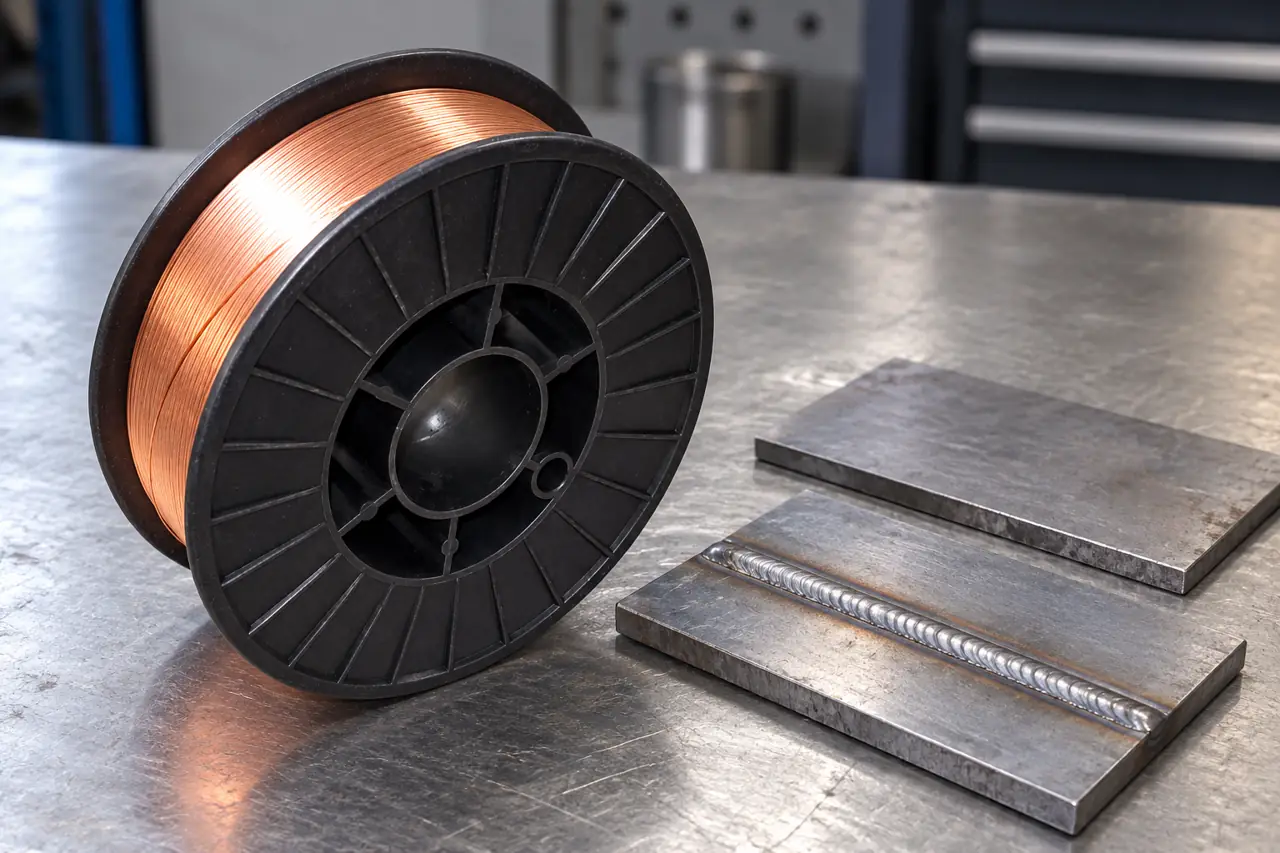
Make the coupon represent fabrication
Use representative parent material, thickness, joint preparation and fit-up. Record wire identity, gas and procedure settings and assess the required bead profile, defects and other joint examinations. A satisfactory appearance can leave required internal or mechanical checks unresolved.
The illustrated coupon bead and spool are AI-assisted examples, not a documented production weld or test result. Retain actual coupons and batch identity with the procedure record. Wire delivery approval and weld acceptance should remain separately visible in the conclusion.
- Actual jointUse representative parent material, thickness, preparation and fit-up for the intended procedure.
- Recorded processKeep wire identity, gas and procedure settings with the retained coupon.
- Required examinationsAssess specified defects and other checks beyond the visible bead profile.
Surface handling should not introduce a new variable
Preserve wire, spool and weld evidence alongside gas and equipment observations before assigning a defect cause.
Protect opened wire against moisture, corrosion, shop dirt and handling damage according to the selected supply and process requirements. Review guide and liner cleanliness where debris appears. A bright copper surface does not measure coating quality or cleanliness.
For a defect, preserve the spool, wire sample and affected weld alongside gas, preparation and equipment observations. Review the evidence before interpreting every porosity, spatter or feeding symptom as a bulk-wire chemistry problem.
- WireSurface and retained sample
- DeliveryTip, liner and feed behavior
- ProcessGas, preparation and settings
- DefectActual weld and location retained
Spool and bulk-pack formats need feeder confirmation
Match spool or bulk-pack geometry and payout to the feeder while defining actual net contents and protection.
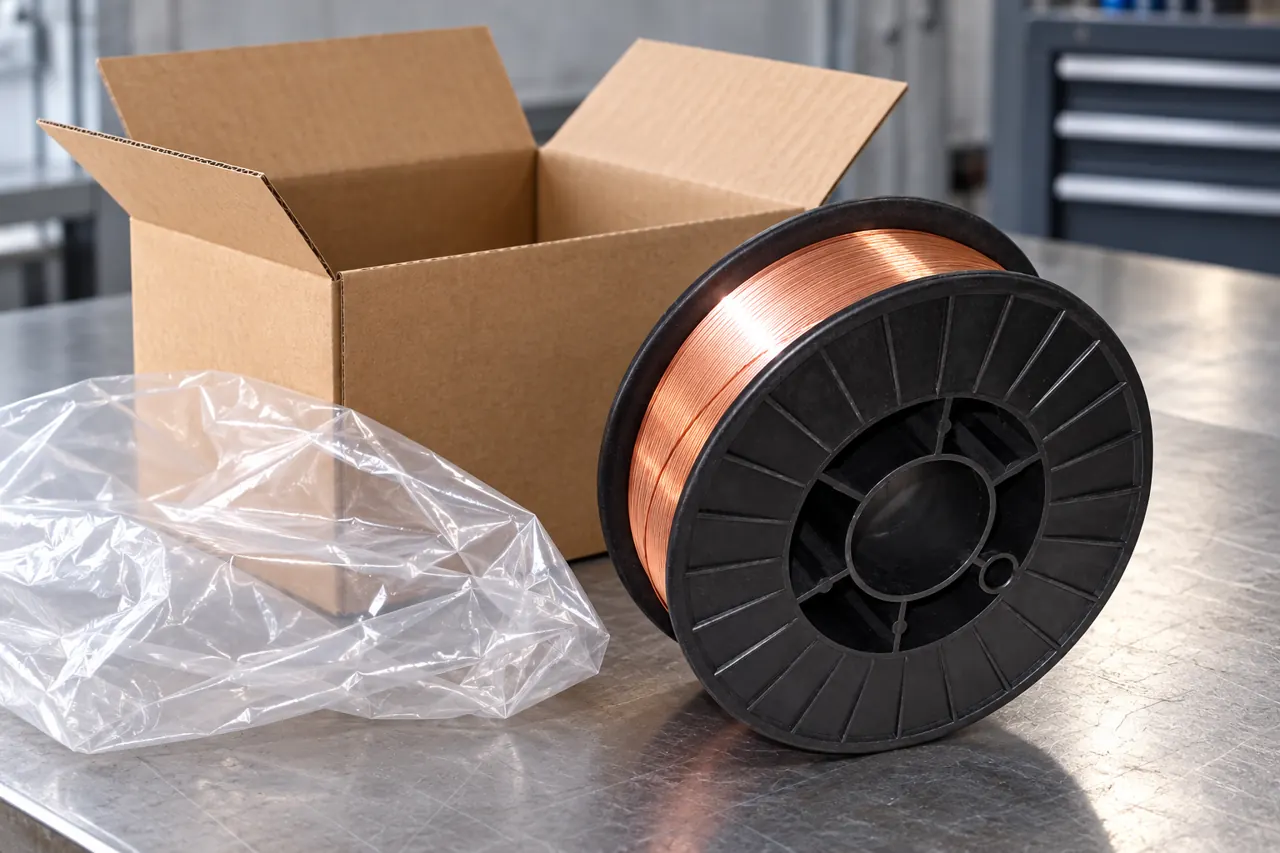
Match the carrier to the feeder
The listing mentions several pack masses, but the actual chosen carrier dimensions, bore, winding and payout must fit your feeder. A bulk pack and small spool can impose different handling and delivery conditions even with the same nominal wire.
The plain carton and spool are AI-assisted packing illustrations. They do not establish a particular unit mass or tested shipping design. Agree net contents, protection, marking and the link to corresponding batch records in the actual offer.
- Spool interfaceConfirm bore, envelope and winding for the actual wire-feeding unit.
- Bulk interfaceDefine payout and handling when a bulk pack is proposed instead.
- Delivery identityAgree net contents, protection and marking linked with the represented batch records.
Repeat supply retains classification and usable delivery
Retain producer, classification, diameter and package when comparing repeat supply and useful accepted weld output.
Keep the approved consumable designation, producer, diameter/limits, surface and pack with the accepted trial and applicable procedure. Review a change in wire source, gas basis, spool or supplied condition rather than replacing by ER70S-6 wording alone.
Compare accepted weld output with feed stops, rejects and rework under comparable conditions. A lower wire price does not prove lower fabrication cost if delivery or joint conformity changes.
- ApprovedProducer, class, size and package
- CompareFeed stops, rejects and useful weld output
- ChangeSource, gas basis or carrier
- ReviewApplicable procedure and evidence
Define the filler and fabrication trial
Send the required filler designation and procedure context so the batch evidence and trial scope can be defined.
Share your required filler designation and the joint procedure you need to preserve. We can review the offered wire package and the evidence needed for a representative trial.
Qingdao Relia Industries Co., Ltd.
Contact address: Shuyuan Road, Qingdao, Shandong, China
- Filler classification and required edition
- Parent material joint and thickness
- Wire diameter and shielding reference
- Feeder and carrier dimensions
- Required records and current defects
Enquiry scope and supporting detail
Send parent grade, joint/thickness, required consumable classification and edition, wire diameter and shielding/process reference. Include feeder/spool constraints, inspection requirements and any current feed or weld defect. Specify the records needed to approve the offered batch.
Request the actual wire and surface identity with corresponding batch evidence and a representative sample format. Add quantity and destination; certification, sample arrangements and current commercial terms require confirmation for the selected consumable supply.
- BaselineProcedure and required classification
- FeedingDiameter and package interface
- TrialSample and inspection scope
- SupplyQuantities and destination