

Arc-Spray Systems for Corrosion-Protection Contractors
Choose an arc-spray system around the coating job, selected wire and site workflow. This guide helps contractors define the complete equipment set, check power and air interfaces, and plan a representative coating trial. You can then compare a supplied configuration against the actual preparation, access and acceptance requirements of the project.
Select the set from the coating job
For a corrosion-protection job, select an arc-spray set from the required coating and site workflow rather than a current-range label alone. Start with substrate, surface preparation, selected metal wire and the coating acceptance your project requires. Relia supplies equipment and selection support; it does not manufacture the spray machine. Send the job geometry and utility brief so the offer can define the actual power source, gun, wire feed and air interfaces, followed by a representative coating trial with responsibilities and evidence stated.
- Coating requirementDefine substrate, wire and the coating acceptance required by the actual project.
- Site workflowDescribe access, reach and workpiece geometry before selecting the equipment arrangement.
- Complete configurationConfirm power source, gun, feed and utilities together in the supplied set.
Selection context and decision detail
| Buyer requirement | Relia response | Evidence / condition |
|---|---|---|
| Project coating requirement | Equipment supply and selection support | Substrate, wire, preparation and acceptance |
| Complete usable set | Actual configuration/interface review | Gun, feed, source, air and site scope |
| Reviewable release | Maker checks plus representative coating trial | Machine function separated from coating results |
The machine offer must define a complete selected set
Confirm the selected set and maker evidence through the equipment supply offer rather than assuming machine manufacture.
Relia supports equipment supply and selection without claiming machinery manufacture. Company incoming, in-process and final QC with corresponding batch records is confirmed. For this equipment, assign actual maker checks, outgoing evidence and commissioning scope; those general QC facts are not a coating-performance result.
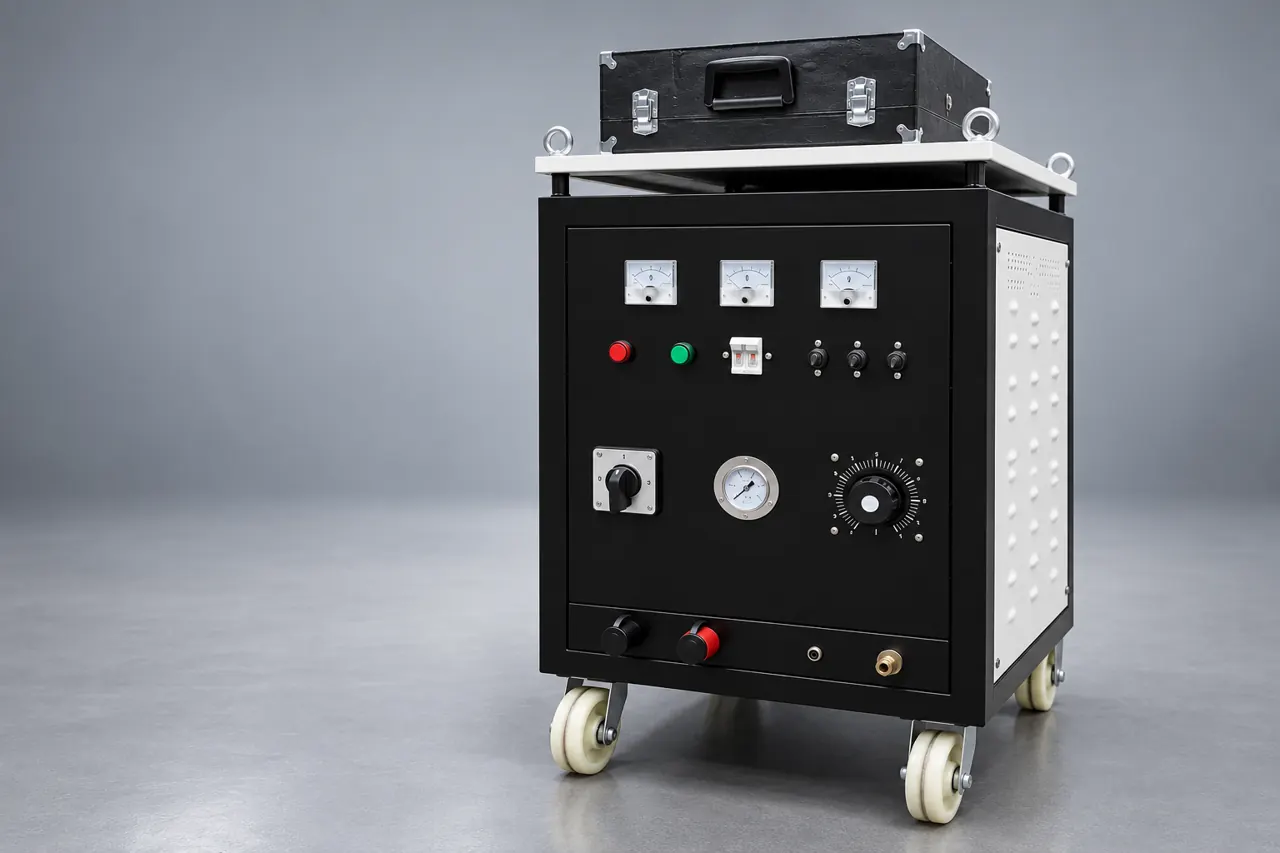
Product 985 has one PT350A–PT600A range label, a 380 V field and 15KVA entered under Power(W). Confirm electrical rating/units, duty and actual configuration. The combined label does not establish separate 350 A and 600 A operating specifications or all included accessories.
- ProjectCoating specification and acceptance
- WorksiteAccess and operating constraints
- UtilitiesActual available connections
- ApprovalResponsible contractor or client authority
Twin-wire arc spraying converts wire into a deposited layer
Twin-wire melting and air atomization depend on coordinated wire delivery, electrical behavior and the selected feed hardware.
How twin-wire arc spraying deposits metal
In the general process, two electrically opposed wires meet at an arc and melt at their tips. An air stream atomizes and carries the metal toward the prepared substrate. Feed and electrical behavior need to remain coordinated for stable operation.
This mechanism explains why wire, guides, drive and air condition belong to one system. It does not establish the offered machine's deposition rate or duty cycle.
- Feed the wiresTwo electrically opposed wires advance to meet at the selected gun arrangement.
- Melt the tipsAn arc melts the wire tips while delivery and electrical behavior remain coordinated.
- Atomize and depositAir carries atomized metal toward the prepared substrate to build the coating.
Product references for your shortlist
Open the product details, then discuss the exact specification for your application.
Arc-spray equipment configuration enquiry
A supply and selection reference for defining the actual arc-spray set around a contractor’s coating job and utilities.
Surface preparation controls a different part of adhesion
Assign surface preparation separately because cleanliness and profile affect adhesion independently of normal machine operation.
The deposited particles meet a cleaned, appropriately roughened surface; contamination or an unsuitable preparation can undermine the coating even when the machine feeds normally. Specify the required cleanliness/profile basis and the interval/condition represented by the trial.
Assign blasting and inspection responsibility separately from machine supply. No automatic adhesion value or universal abrasive/preparation recipe is implied.
- Prepare the surfaceProduce the specified clean and roughened condition on the substrate selected for the trial.
- Verify starting conditionUse the agreed cleanliness and profile basis with preparation and inspection responsibility assigned.
- Run represented coatingPreserve the relevant interval and surface condition when assessing the deposited coating.
Wire selection should match both service and feed hardware
Choose wire for the coating design, then verify diameter, condition and feed format against the gun and drive.
Choose the metal/alloy from the coating design, then verify actual diameter, condition and feed format against the gun and drive. Zinc, aluminium and zinc-aluminium are not interchangeable solely because all are corrosion-protection candidates.
Keep wire chemistry and physical feed evidence with the selected setup; the machine cannot correct an unidentified consumable.
- Coating materialChoose the metal or alloy required by the coating design and intended service.
- Physical wireConfirm actual diameter and supplied condition against the selected gun and wire drive.
- Feed formatAgree the delivery package and retain chemistry evidence with the actual spraying setup.
The set boundary should include every process interface
Itemize gun, feed, connections and utilities so the offer defines a working set beyond the power cabinet.
Define equipment and site interfaces
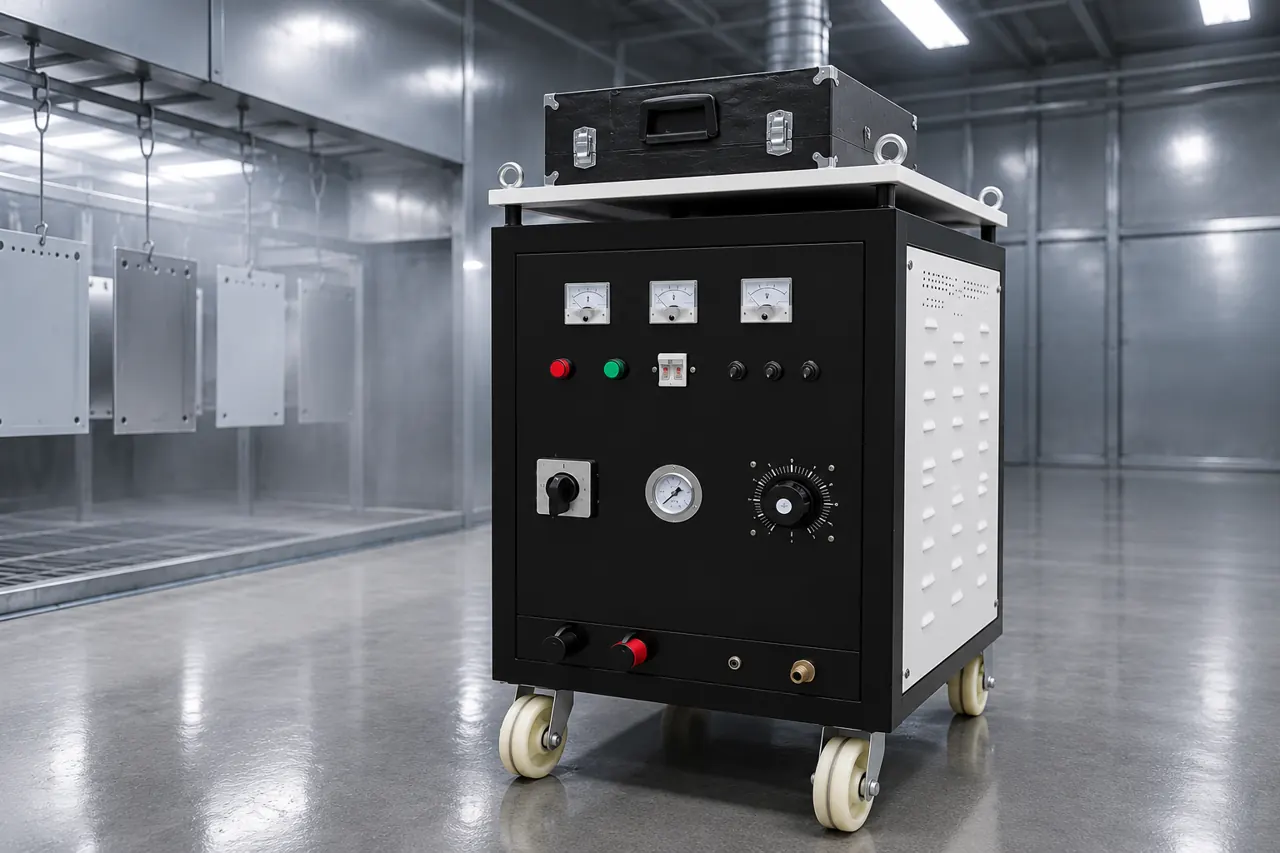
List the actual gun, feed unit, cables/hoses, controls, wire handling and required air treatment or other utilities. Identify supplied items and site-provided interfaces explicitly.
The cabinet-only illustrations show a power-unit concept. They do not show the gun/feed arrangement or prove that a complete working package is supplied.
- Included hardwareItemize the actual gun, feed unit, controls, cables and hoses in the offer.
- Wire handlingConfirm the wire format and delivery arrangement matched to the selected feed system.
- Site utilitiesIdentify required power, air treatment and other connections supplied by the worksite.
A job-shaped trial is more informative than a flat easy panel
Trial representative access and geometry, recording coverage and other required coating checks under their own methods.
Use representative substrate and preparation plus the selected wire and actual geometry, including difficult access or edges where relevant. Record operating conditions, passes and the agreed coating checks.
Separate thickness/coverage, adhesion or other required assessments under their own methods. A visually uniform metallic surface does not establish every numerical result or corrosion-service interval.
- Actual geometryInclude representative substrate, difficult access and relevant edges in the trial piece.
- Prepared inputUse the selected wire and required preparation while recording operating conditions and passes.
- Separate resultsAssess coverage, thickness and any required adhesion through their own agreed methods.
Factory checks and field coating acceptance need different records
Keep equipment functional checks distinct from commissioning and the project’s coating acceptance evidence.
Confirm equipment identity and functional checks, then define commissioning and the project's coating acceptance with assigned parties. A maker test report can concern the machine; a coated coupon concerns a represented process condition.
Do not treat CE wording, portability or an anticorrosion application label as verified compliance, deposition output or coating life.
- Maker checksConnect equipment identity and functional checks with the actual selected machine configuration.
- Commissioning scopeAssign the site responsibilities and records for bringing that set into operation.
- Coating acceptanceUse the represented coated sample and project methods to judge the process result.
Site practicality depends on utilities and handling
Review electrical supply, air, reach and movement for the complete site layout rather than the cabinet alone.
Check the working layout before selecting the set
Agree the actual electrical supply, air quality/flow requirements, cable reach, movement and workpiece access for the chosen configuration. Nominal cabinet dimensions and mass do not establish the whole working layout.
Confirm extraction and operating provisions through the selected machine/site documentation, with training and consumables support defined in the offer.
- Electrical interfaceConfirm actual site supply against the selected configuration’s rating and connection requirements.
- Air and reachReview air requirements, hose and cable reach for the actual coating locations.
- Worksite arrangementPlan movement, access and operating provisions from the selected equipment and site documentation.
Describe the coating job and worksite
Send coating requirements and site interfaces together to define the selected equipment, trial and support scope.
Send the coating specification and available utilities so we can discuss a selected equipment set, representative trial and clearly assigned commissioning responsibilities.
Qingdao Relia Industries Co., Ltd.
Contact address: Shuyuan Road, Qingdao, Shandong, China
- Substrate geometry and access conditions
- Coating specification and wire alloy
- Preparation and coating acceptance methods
- Site electrical and air interfaces
- Required gun feed and connection scope
Enquiry scope and supporting detail
Send substrate and geometry, intended wire/alloy, preparation requirement and coating acceptance methods. Add site power/air, access, reach and production pattern. We can then define a selected set, maker and trial package with commissioning and documentation responsibilities, before quantity, service and delivery conditions are agreed.
- TechnicalProject · wire · utilities
- ConfigurationMachine · accessories · interfaces
- ContractAcceptance · support · delivery