Steel wire feedstock for welded mesh production lines
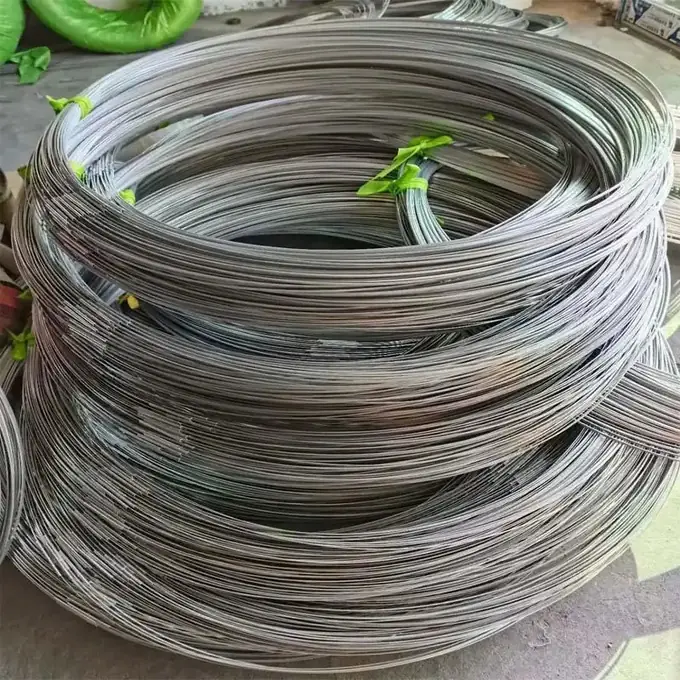
Match feed wire to the complete mesh production route, including welding and any later coating. A galvanized wire listing and an annealed carbon-wire listing describe different starting conditions. We can review both against your line requirements; acceptance should follow a feeding and welding trial that represents your actual production sequence.
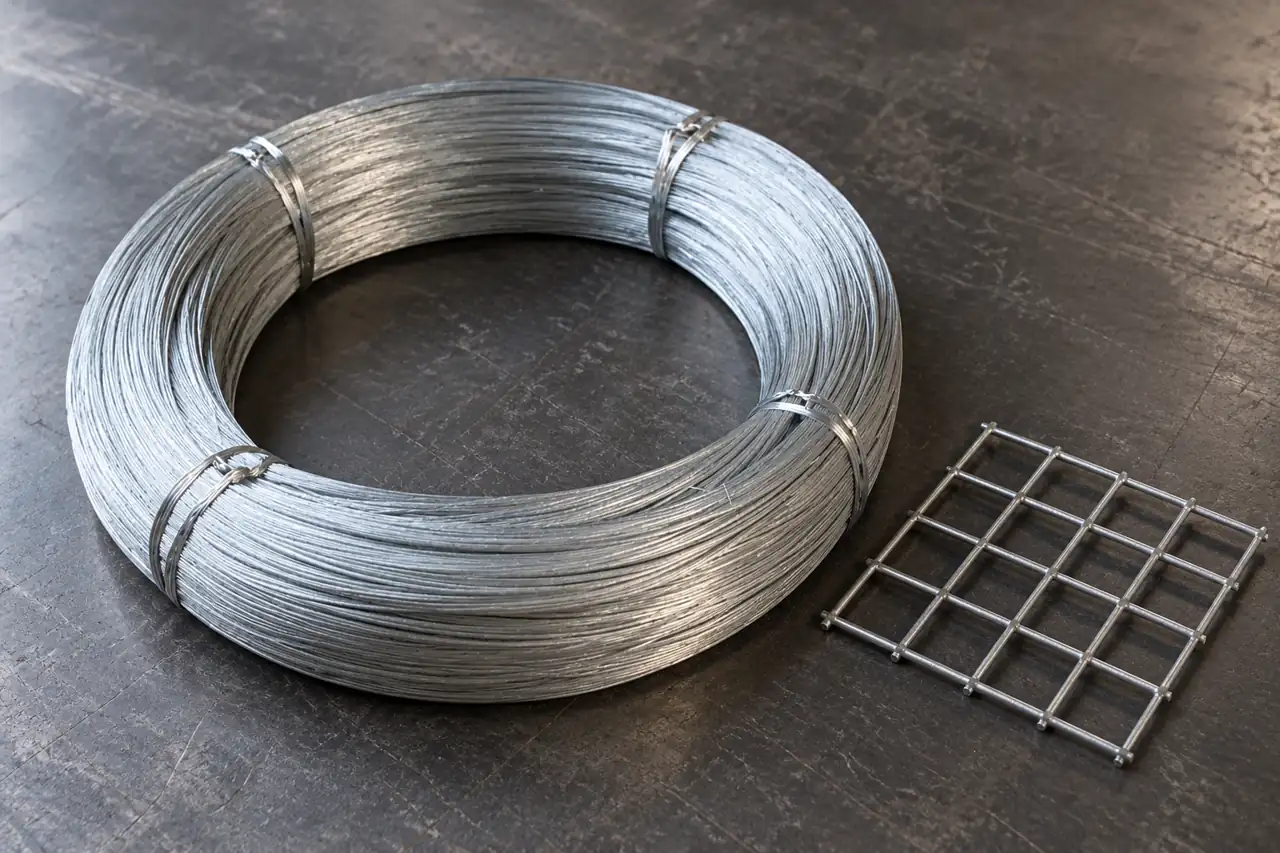
Draw the welding and coating sequence
State whether the wire is coated before welding, whether the mesh is treated after welding, or whether another route applies. Each sequence changes what must be evaluated at the weld and on exposed surfaces. Do not allow a quotation to replace your intended route with an assumed interpretation of galvanized mesh.
Specify diameter and supplied condition together
Diameter tolerance, tensile condition and surface condition belong on the same feed-wire specification. Include how the line straightens and feeds the wire, and distinguish longitudinal supply from cross-wire preparation. A nominal wire size alone cannot establish feeding behaviour or the consistency of the finished aperture.
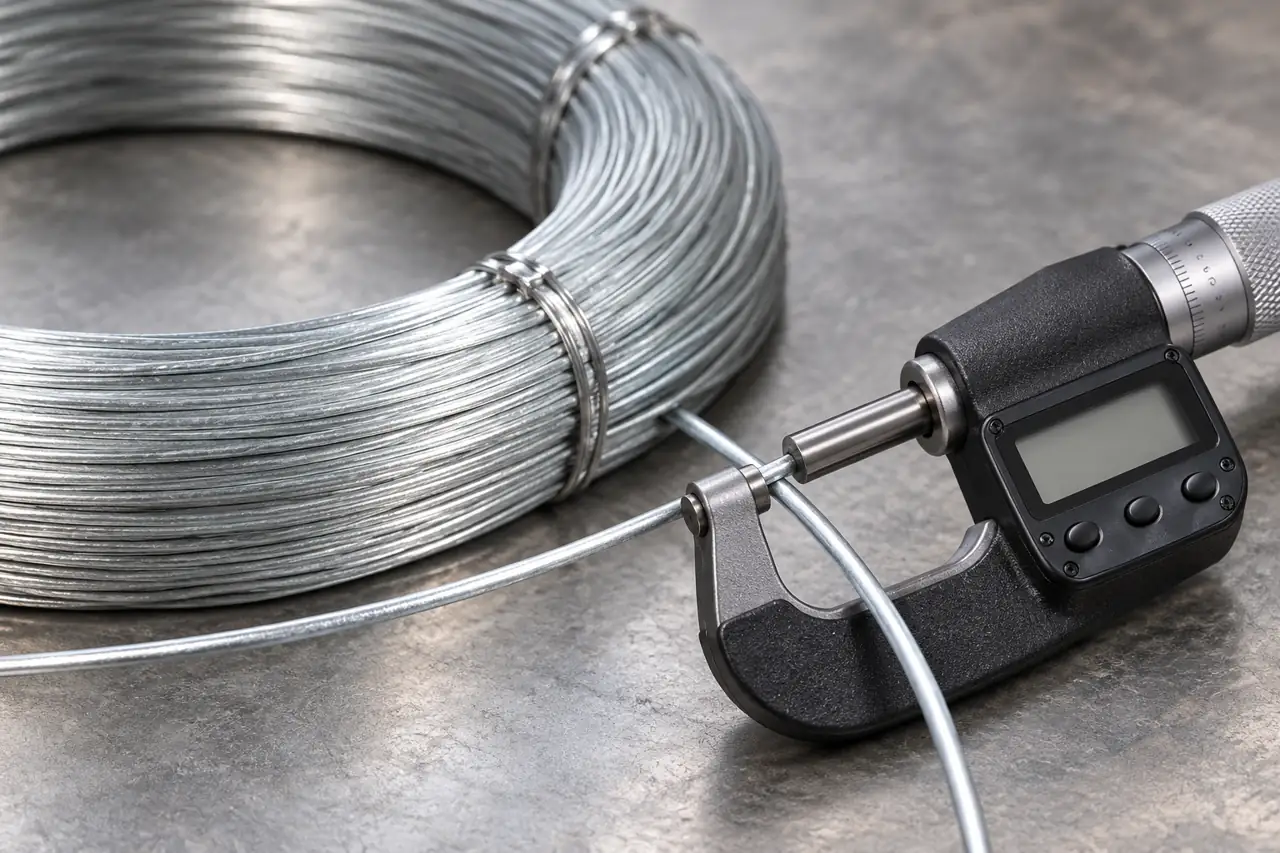
Test the wire in the intended welding process
Use production-representative wire and identify the trial coil. Record the machine settings, joint checks and any coating observations required by your mesh specification. Welding acceptance must be agreed with your technical team; an attractive mesh panel is not sufficient evidence that every joint meets the intended service requirement.
Set coil dimensions around the payoff
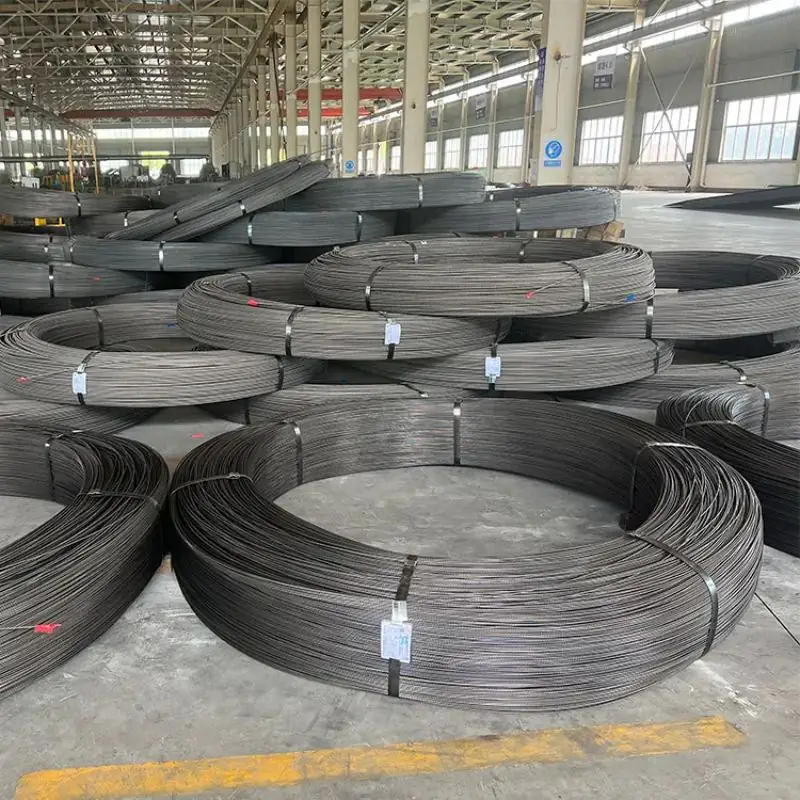
Provide the payoff arrangement, permitted coil dimensions, mass limits and tying or spool requirements. Incorrect winding or an unsuitable package can interrupt a line even when the wire itself meets its material specification. Ask for the proposed format in writing and inspect it before scheduling a sustained production run.
Inspect before assigning a production slot
Check package condition and lot identity first, then compare diameter and the agreed surface condition with the order. Retain any material documents beside the trial record. If the incoming wire differs from the approved sample, isolate it for review before that difference becomes a welding adjustment made on the production floor.
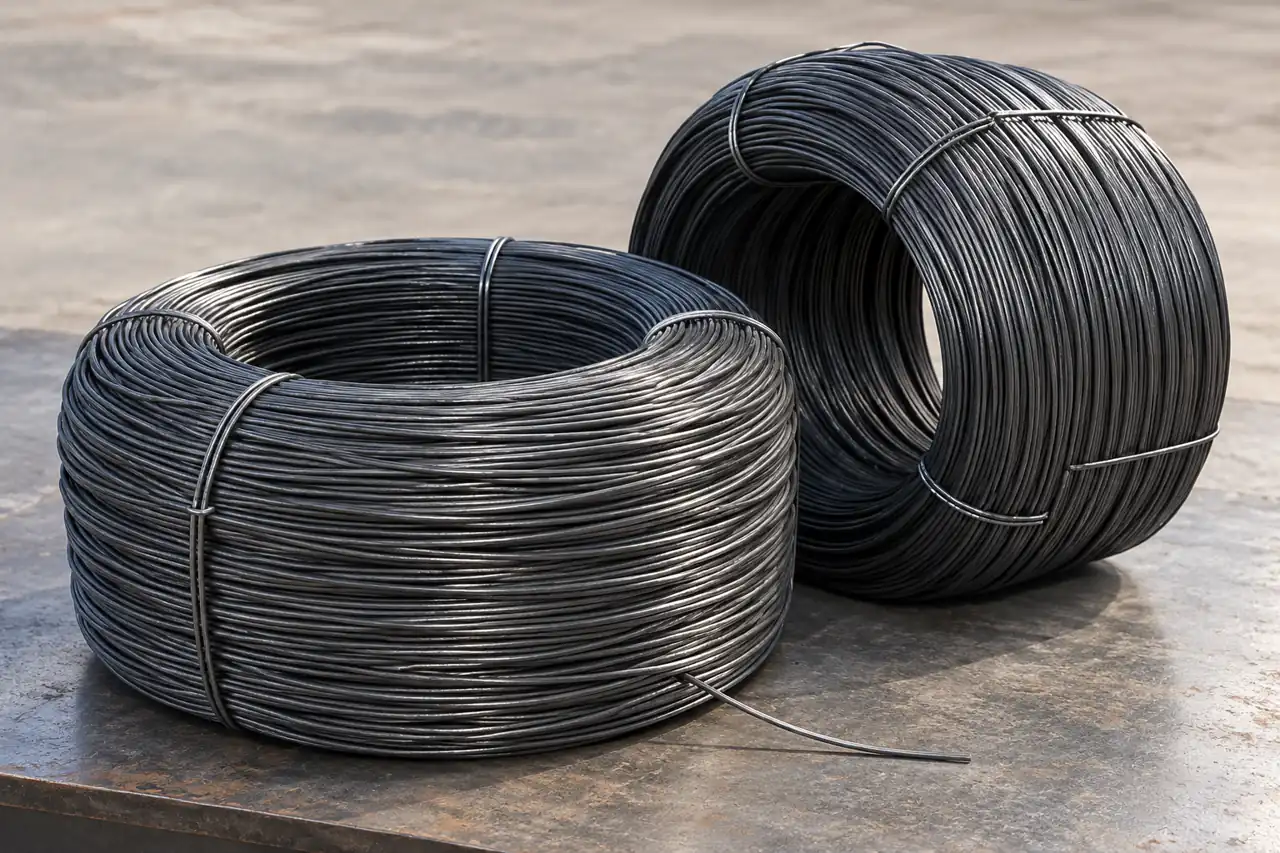
Distinguish feed wire from finished mesh
This enquiry concerns wire entering your manufacturing line. Finished mesh panels or rolls require their own aperture, dimensions and weld acceptance, and should not substitute for a feedstock quotation. Our catalogue references provide a starting point; the final proposal needs to identify the wire condition and supply responsibility for your process.
Keep trial coils and shipment coils linked
Agree how the approved wire specification will appear on coil labels and shipping documents. Protect winding during handling and keep different diameters or surface conditions separated. A receiving team should be able to match each coil to its order line without relying on colour or appearance, particularly when similar wires share a shipment.
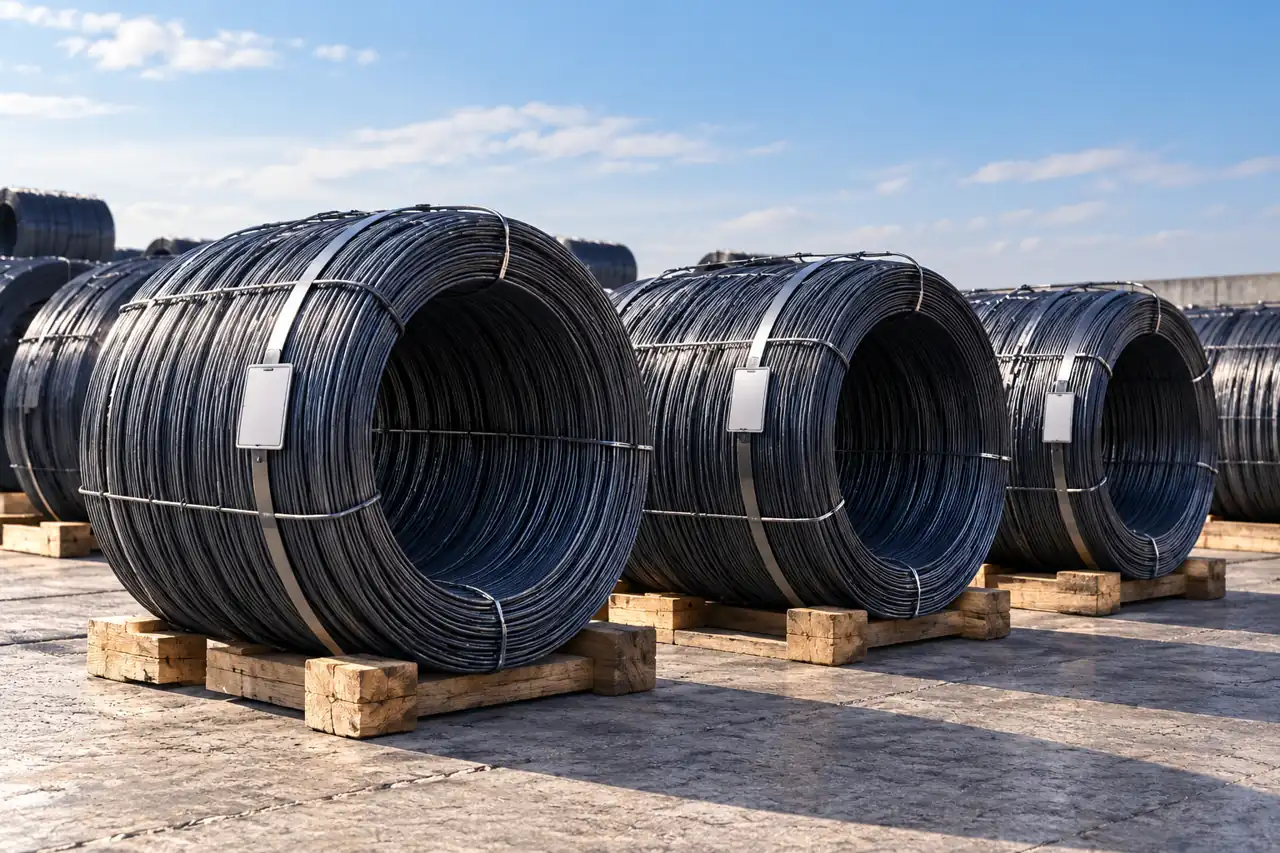
Track changes through the repeat order
Repeat supply should reference the approved wire condition, coil format and welding trial. Ask for notice of a change to material route or supplied surface before treating it as equivalent. If weld consistency changes, compare both incoming wire evidence and recorded machine conditions so the investigation stays grounded in the actual production run.
Send a route-based feed-wire enquiry
Tell us your mesh application, welding equipment, wire sizes, required condition and coating sequence. Add the payoff format, initial trial quantity, ongoing demand and destination. We can review relevant wire catalogue entries and confirm the proposed specification, documentation and commercial terms for your line before a volume order is considered.